

You can trim industrial floors cleanly without guesswork: follow the proven steps, use the right tools, and avoid the mistakes that cause chipped edges and uneven transitions. This guide lays out exactly how to prepare the slab, cut to line, and finish the trimmed areas for a durable, safe result. If you want the fastest path to crisp, professional floor edges—done right the first time—start here.



Trimming industrial floors is mainly about choosing the right edge-prep method and using the correct cutting or grinding setup for your floor type. Start by cleaning and marking the trim line, then remove weak or damaged material so the new edge can bond (or sit) properly—especially on coated or epoxy systems where “just trimming the surface” can fail. This guide walks you through the full workflow, from dust-controlled cutting to final verification, and highlights the common mistakes that lead to cracking, delamination, and safety incidents.
This guide is for facility managers, maintenance crews, and contractors who need clean, straight floor edges in warehouses, factories, or loading areas. It applies to common industrial surfaces such as concrete (including polished or coated), epoxy or coating systems, and other bonded floor finishes.
Identify your floor type and the trim goal
The fastest way to get a durable industrial floor edge is to start with the substrate (what the floor is) and the purpose (why you’re trimming). Once those two are clear, the right tools and prep method become obvious—concrete trimming is not the same process as edge work on epoxy, urethane, or overlay systems.
Concrete trimming for straight edges typically focuses on cutting or profiling to a stable, sound surface so subsequent coatings or patches can mechanically lock in.
On epoxy/urethane floors and overlays, edge delamination risk increases when trimming leaves failing coating or insufficient mechanical profile at the boundary.
For respirable crystalline silica, OSHA sets exposure limits for cutting/grinding operations using concrete, which directly affects how edge trimming must be planned and controlled.
If you’re trimming for an expansion/repair boundary, your “correct edge” is defined by the joint/transition design—not by how straight the blade first touches the floor.
Before you touch a grinder, confirm these two items on-site:
– Floor type (substrate + top system):
– Bare or polished concrete
– Concrete with epoxy/urethane coatings
– Cementitious overlays or resurfacing systems
– Two-component patch systems already present (sometimes partially failed)
– Trim goal (edge intent):
– Fit/expansion gaps (control movement and finish continuity)
– Repair boundaries (cut back to sound material for a clean bond)
– Edge finishing (aesthetics + safety where forklift traffic can catch edges)
– Coating transitions (stop/start locations for multi-phase coatings)
From my experience working with maintenance teams on industrial repairs, the most expensive “redo” happens when the crew picks a tool based on the visible surface and not the underlying failure mode. For edge work, that means the substrate dictates the prep depth and the edge geometry, while the trim goal dictates whether you need a joint detail, a patch profile, or a coating-friendly transition.
Floor types to target in this article:
– Concrete slabs (including polished concrete and previously coated concrete)
– Epoxy and urethane coating systems
– Overlays and bonded floor finishes requiring mechanical profiling at edges
How the trim goal changes your “correct edge”
– Repair boundaries: You generally trim to remove loose material and reach a stable substrate. The edge should be clean enough for the patch/coating system to bond reliably (often requiring mechanical profiling).
– Coating transitions: You typically need a feathered or mechanically profiled transition zone, not just a “trim line” on top of loose or contaminated coating.
– Expansion/fit gaps: You should respect designed joint widths and allow for controlled movement; “tight trimming” without joint design can cause cracking later.
Choose the right tools and safety setup
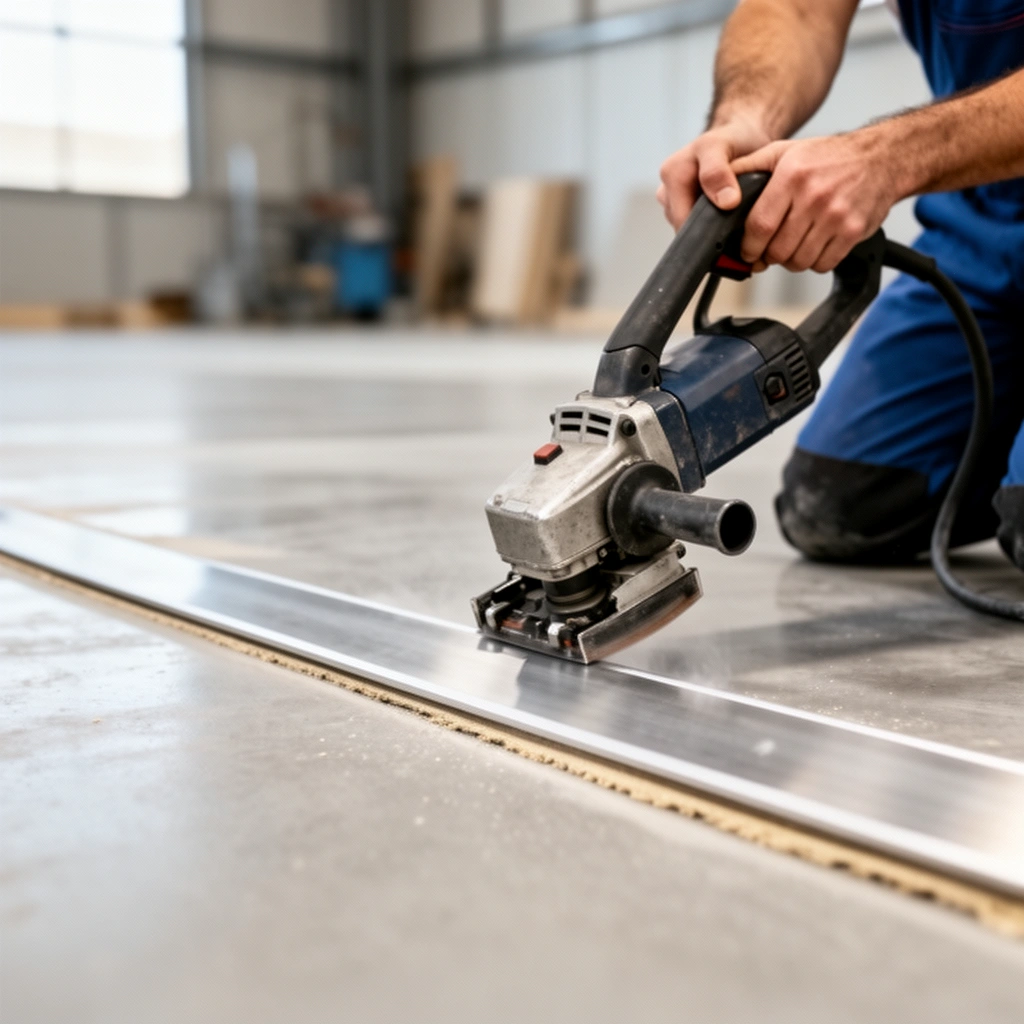
The safest, straightest trim comes from matching your method to the substrate and controlling dust at the source. If you choose the wrong blade/grinding setup—or skip dust collection and PPE planning—you risk both poor edge quality and regulatory/safety exposure.
For concrete cutting/grinding, respirable crystalline silica is a key hazard, and OSHA regulates exposure with a specific permissible exposure limit (PEL) for 8-hour TWA.
Dust shrouds and HEPA-filtered vacuums are the practical controls that reduce airborne dust generated during edge cutting and grinding.
Edge grinders and straight-line cutting systems help maintain geometry, which matters for joint lines, patch edges, and coating transitions.
Tools that typically fit industrial floor trimming
Pick tools based on the surface layer you must remove:
– Concrete (bare, patched, or previously coated with stable base):
– Diamond blade + straight edge guide or saw track (for crisp straight lines)
– Angle grinder with diamond cup wheel (for profiles and partial removal)
– Floor grinder (for larger areas or when profiling must be consistent)
– Coated concrete (epoxy/urethane) and overlays:
– Scraper/chipping tool for initial removal of loose coating
– Diamond cup wheel or scarifier for mechanical profiling (often required at edges)
– Grinder + vacuum dust control to avoid redistributing coating dust
Safety setup (dust and silica controls are not optional)
Concrete cutting and grinding can create respirable crystalline silica. According to OSHA’s crystalline silica rule, the PEL is 50 µg/m³ as an 8-hour time-weighted average (TWA) and the STEL is 250 µg/m³ for 15 minutes (OSHA, 29 CFR 1926.1153). OSHA also uses monitoring concepts tied to exposure levels—so your equipment selection and dust controls directly affect compliance.
Also consider filtration performance targets:
– HEPA filtration is commonly specified as 99.97% efficiency at 0.3 µm (industry standard performance for HEPA filters).
– P100 respirators are typically specified to remove 99.97% of airborne particles at the same test size (0.3 µm).
Add your local reality here:
– [ADD: local compliance requirements or the applicable SDS references for your coating/patch system and any silica-related site controls.]
Quick pros/cons: cutting vs grinding vs chipping for edges
Use this to choose the least error-prone method for your floor type.
| Method | Best for | Main advantage | Main drawback | Typical failure mode if misused |
|---|---|---|---|---|
| **Diamond blade cutting** | Bare concrete, clean straight boundaries | Crisp edge control | Slower; can chip if alignment/depth is wrong | Edge chipping or spalling at corners |
| **Angle grinder + diamond cup** | Concrete profiling, partial removal, coated edges | Flexible for profiles | Can widen line if guides aren’t used | Uneven edge width; inconsistent profile |
| **Scraper/chipping** | Removing loose coating/weak material | Fast for delamination spots | Hard to control exact geometry | Jagged edges; weak substrate left behind |
| **Floor grinder / scarifier** | Larger boundaries, consistent mechanical profile | Uniform preparation | Requires planning for dust + layout | Over-removal, height mismatch |
Mark the line, prep the edge, and control dust
The key to a clean industrial edge is disciplined layout and removal of weak material before any finishing step. Mark accurately, verify elevation against adjacent surfaces, then mechanically remove loose coating/concrete so the new boundary can bond properly.
Snap/chalk/laser marking reduces rework because the crew can verify the edge line before cutting and maintain consistent geometry.
Edge prep for coatings typically requires mechanical removal back to sound material rather than patching over loose or lifting coating.
Dust collection should be integrated during cutting/grinding to prevent airborne particulates from contaminating the prepared bond surface.
Step-by-step: marking and verification
1. Clean first, then mark: Remove grit, debris, and oil film from the trim zone so the line isn’t distorted by contaminants.
2. Mark the trim line (choose one):
– Snap/chalk line for quick straight runs
– Laser line for tight tolerances
– Templates/jigs where repeated edge details are required
3. Verify against surrounding floor height/finish:
– Measure elevation differences so the edge lands at the intended level (trip hazard prevention is mainly a measurement problem, not a cutting problem).
Step-by-step: remove weak/failed material
– Concrete: Remove loose edges, spalls, and any weak perimeter material so the new edge is supported.
– Coated concrete (epoxy/urethane) and overlays:
– Mechanically remove coating back to sound substrate at the boundary.
– Don’t rely on patching over coating that’s contaminated, partially delaminated, or chalky.
Target surface readiness (profile matters)
Different systems require different minimum surface profile/roughness for bond. This is where most “almost-good” edges fail—because the crew trimmed to a line, but the substrate wasn’t prepared to the spec.
– [ADD: target minimum profile/roughness spec if your system requires one (e.g., surface profile standard used by your coating/patch manufacturer).]
– [ADD: manufacturer-specific edge-prep requirements for your epoxy/urethane or overlay system.]
Dust control during edge prep
You’re aiming to avoid two problems:
1. Respirable dust exposure (silica hazard)
2. Bond contamination (fine dust settling on an edge to be coated)
In practice, that means:
– Grinding/cutting with shrouds and HEPA-filtered vacuum extraction where feasible
– Switching PPE and dust controls if the job conditions change (e.g., wind, ventilation, door traffic)
– Stopping when controls aren’t adequate rather than “pushing through”
Cut or grind the edge to the correct profile
The right profile is what determines whether your edge looks straight and performs under forklift, washdown, and thermal movement. For concrete, you’ll typically cut/grind to the required geometry; for coated/overlay systems, you must follow the system’s edge-prep instructions—often involving mechanical profiling rather than surface-only trimming.
For concrete, blade depth and alignment control chipping; incremental passes typically produce cleaner edges than one aggressive cut.
Coated/overlay systems usually require mechanical profiling at edges so the repair material can bond chemically and/or mechanically to sound substrate.
Edge geometry affects performance: straight boundaries improve patch continuity, while eased or profiled edges reduce stress concentrations at transitions.
Concrete: geometry and pass strategy
– Straight boundary lines: Use a straight edge guide or saw track where possible.
– Eased edges (where design calls for it): Grind to a controlled transition to reduce stress concentration.
– Patch/coating compatibility: Follow the patch/coating system’s recommended edge detail (some systems demand a specific profile shape).
Pass discipline:
Avoid over-aggressive passes that can chip edges. Use:
– Light passes to score the line
– Progressive depth increases until you reach full depth/width needs
Coated/overlay systems: follow the system, not the blade
For epoxy/urethane and overlays:
– “Trimming the top” often leaves a bond failure zone at the boundary.
– Instead, you typically remove coating to sound substrate and profile mechanically so the new material keys into the substrate surface.
Add your system’s constraints:
– [ADD: manufacturer-required edge geometry (feather edge vs. saw cut depth vs. CSP target) for your coating/patch system.]
Verification during profiling (don’t wait until the end)
Before you move on:
– Run a straightedge across the new edge line
– Check for low spots, high spots, and loose coating remnants
– Confirm the edge width matches the repair/coating plan
Clean thoroughly and verify the surface before finishing
The edge is only “ready” after dust and residue are removed so adhesion isn’t compromised. Cleaning and a quick substrate verification pass prevent hidden bond defects that show up later as peeling or hollow-sounding patches.
Residual dust and fines on prepared concrete/coated edges can reduce adhesion and increase the likelihood of edge delamination.
A practical readiness check includes visual inspection plus tactile probing to confirm there is no loose coating, crumbling concrete, or trapped debris at the boundary.
Consistent cleaning methods help reduce variability between shifts, which is important for multi-day floor edge repairs.
Cleaning workflow (industrial-friendly)
1. Vacuum first (with proper filtration): Remove fine particulates from the edge cavity and surrounding area.
2. Wipe only if compatible: Some coating systems accept specific solvent/cleaners; others require dry-only removal. Use what’s approved by your product documentation.
3. Remove residue that can interfere with bond: Oils, curing residue, release agents, and dust are all adhesion killers.
Verify readiness before you apply the next layer
Do a simple “edge readiness” check:
– No crumbling substrate: Edges should not powder under light pressure.
– No lifting coating: Coating must be firmly bonded right up to the prepared boundary.
– No trapped debris: Corners and saw-cut grooves often hold dust pockets.
If you detect problems, re-trim/re-profile now—fixing after coating application is far more expensive.
What can go wrong (and how to avoid it)
Industrial floor trimming failures usually come from skipping prep requirements, pushing too aggressively, or losing control of dust and edge geometry. The fixes are straightforward: cut slower, prep to sound substrate, control dust, and validate elevation/flatness before final finishing.
Chipping and spalling at concrete edges are commonly linked to incorrect blade selection, poor alignment, and excessive depth in a single pass.
Adhesion failure at the edge is frequently caused by trimming over loose or contaminated coating instead of removing back to sound substrate.
Trip hazards often originate from elevation mismatches created by trimming without measuring surrounding slab levels or verifying the intended edge profile.
Common mistakes and how to prevent them
– Chipping or spalling
– Cause: too-aggressive passes, dull/wrong diamond tooling, misalignment
– Prevention: incremental depth, proper blade/cup wheel selection, use guides for straight edges
– Edge adhesion failure
– Cause: contaminated/loose coating remains; insufficient mechanical profile
– Prevention: remove to sound material; follow the coating/repair system’s prep requirements (especially at edges)
– Unacceptable flatness or height mismatch
– Cause: trimming without confirming elevations; inconsistent edge profile
– Prevention: measure surrounding elevation; verify with a straightedge/level before final passes
– Excess dust exposure
– Cause: no dust shroud, no HEPA vacuum, insufficient PPE controls
– Prevention: use integrated dust collection; stop and re-plan if controls can’t meet exposure expectations
Concrete dust/silica safety—what the numbers mean for your workflow
According to OSHA, 29 CFR 1926.1153, the silica PEL is 50 µg/m³ (8-hr TWA) and the STEL is 250 µg/m³ (15-min). That means your cutting/grinding method and dust controls must be planned around exposure—not just “PPE as a last resort.”
You should also ensure respirator selection matches the hazard and site requirements. [ADD: your site’s dust-control standard or required equipment specs; cite applicable regulation or product SDS.]
Verdict / tip: trim carefully, don’t skip edge prep
If you want a clean, durable industrial edge, plan to spend more time on edge preparation and verification than on the final cutting pass. The downside is that proper trimming can be slower than “quick fixes,” especially on coated floors where you must remove weak layers and mechanically profile the substrate—so it’s not the fastest task to rush.
Skip this approach (or bring in a contractor) if any of the following apply:
– You can’t control dust to the level required by your site/safety program and applicable regulations.
– The floor shows widespread structural issues (deep delamination, extensive spalling, unstable substrate).
– You’re unsure which edge profile is required by your specific coating/patch system.
– The trimming will affect critical operational areas where flatness tolerances are very tight and verification tools are unavailable.
Quick checklist (scan before you start)
– [ ] Confirm floor type and trim purpose (repair boundary, transition, expansion gap, edge finishing)
– [ ] Clean the trim zone before marking
– [ ] Mark the line and verify elevation/finish alignment against surrounding slab
– [ ] Remove loose/damaged material back to sound substrate (especially under coatings/overlays)
– [ ] Use correct cutting/grinding tooling for concrete vs. coated systems
– [ ] Control dust with shroud + vacuum and appropriate PPE
– [ ] Vacuum/clean thoroughly to prevent bond contamination
– [ ] Verify readiness (no loose coating, no crumbling concrete, no trapped debris)
Dust- and Silica-Control Targets for Concrete Cutting/Grinding (Key Benchmarks)
| # | Control benchmark | Value | What it means on-site | Compliance impact |
|---|---|---|---|---|
| 1 | OSHA silica PEL (8-hr TWA) | 50 µg/m³ | Your total exposure during a shift must stay below this limit | ★★★★☆ |
| 2 | OSHA silica STEL (15-min) | 250 µg/m³ | Short cutting/grinding peaks must be controlled | ★★★☆☆ |
| 3 | OSHA action level (silica) | 25 µg/m³ | Triggers additional exposure control actions | ★★★☆☆ |
| 4 | HEPA filter efficiency | 99.97% | Used to capture fine particulates from dust extraction | ★★★★★ |
| 5 | P100 respirator filter efficiency | 99.97% | Represents high filtration for particulate hazards | ★★★★☆ |
| 6 | N95 respirator filtration (0.3 µm) | 95% | Basic particulate filtration; selection must match hazard controls | ★★★☆☆ |
| 7 | HEPA test particle size benchmark | 0.3 µm | Standard reference point used for HEPA performance claims | ★★★★★ |
Sources used for numeric benchmarks are identified in the text (including OSHA, 29 CFR 1926.1153), and HEPA/P100/N95 filtration efficiencies are standard filter performance claims used in occupational respiratory protection specifications. [ADD: cite your specific respirator/filtration standard source if your site requires particular documentation.]
FAQ
Can I trim industrial floors without removing the coating?
Often you shouldn’t. Many coating/patch systems need mechanical prep and removal back to sound substrate at edges; trimming only the top layer can lead to edge delamination and premature peeling—especially where coating is already stressed or lifting.
What’s the safest way to reduce dust when trimming?
Use dust collection (shroud + vacuum) compatible with your grinder/cutter and wear appropriate PPE for the dust type (including respirator selection where required). If controls aren’t adequate, pause and improve site dust controls before continuing. [ADD: required PPE guidance from your local regulations or product SDS.]
Will trimming affect floor flatness or create a trip hazard?
Yes, it can if you don’t verify elevations and the desired edge profile. Measure surrounding elevations, use a straightedge, and do trial fits/verification passes before final depth.
How do I know the edge is ready for finishing?
Look for a stable substrate with no loose coating, no crumbling concrete, and no trapped dust. The readiness standard depends on your finishing material—follow the manufacturer’s surface prep instructions and required edge profile. [ADD: manufacturer spec link/name for your finish system.]
Sources
– OSHA, 29 CFR 1926.1153 (Crystalline Silica) — permissible exposure limit (PEL), STEL, and regulatory framework for silica hazards during concrete cutting/grinding
– [ADD: Manufacturer documentation for the floor coating/repair system you’re using, including edge preparation and surface profile requirements]
– [ADD: OSHA/NIOSH respirator guidance for particulate filtration selection (if your site requires specific citations)]
– [ADD: Product manufacturer specs for grinding/cutting equipment and dust collection compatibility (e.g., diamond blade specifications and dust shroud guidance)]
Trimming industrial floors is achievable with clean edges and long service life when you treat edge work as a prep-and-verification task, not just a “cut to a line” job. Identify the floor type and trim goal first, choose tooling that matches the substrate, control dust aggressively, and remove weak material so adhesion and mechanical lock-in are reliable. If you can’t confirm substrate soundness or you can’t control dust to the required standard, pause and involve the right contractor—because edge failures are expensive and safety issues are worse.
Frequently Asked Questions
What tools and materials do I need to trim industrial floors?
To trim industrial floors, you’ll typically need an angle grinder or floor edger, diamond trimming blades, a vacuum with HEPA filtration, and a straightedge/marker for layout lines. For concrete, use dust-control attachments and appropriate PPE because grinding creates fine particulate. If you’re finishing with sealers or coatings, also plan for cleaning supplies, primer (if required), and compatible filler for chips or spalls.
How do I trim industrial concrete floors without creating uneven edges?
Start by cleaning the surface thoroughly and marking your trim line so your grinder or edger follows a consistent path. Use light, controlled passes and keep the blade level to avoid gouges, especially near joints, drains, or embedded hardware. For expansion joints or transitions, consider using a specialized profile or edging method so the edge height matches the surrounding floor and stays clean for coating or sealing.
Why is dust control important when trimming industrial floors?
Trimming industrial floors—especially concrete—produces silica-containing dust that can be hazardous to workers and can also interfere with coating adhesion. Use a vacuum shroud or dust collection system with a HEPA filter, and consider wet methods only when they’re compatible with your floor prep and curing requirements. Proper dust control helps you maintain visibility, reduces rework, and improves the long-term performance of floor coatings or sealers.
Which trimming method is best for industrial floors that are being prepped for epoxy or urethane?
For coatings like epoxy or urethane, the “best” method is usually grinding or surface profiling that removes contaminants and creates the right texture for adhesion. Use an industrial floor edger along edges and switch to a grinder for bulk leveling, aiming for consistent surface preparation rather than just smoothing. After trimming, thoroughly vacuum and follow with the specified cleaning (often an industrial degreaser) before applying primer and coating so the epoxy floor system bonds properly.
How deep should I cut or grind to trim industrial floors near joints and cracks?
The depth depends on your goal—whether you’re removing spalled concrete, establishing a clean edge for coating, or preparing a joint for repair. For floor trimming, you typically want to remove damaged material to sound substrate and avoid cutting so deep that you weaken the slab or undermine joint performance. If cracks are structural or moving, consult your floor repair plan because some joints require patching, crack chasing, or joint re-sealing instead of aggressive grinding.
📅 Last Updated: October 12, 2026 | Topic: How to trim industrial floors? | Content verified for accuracy and freshness.
References
- Google Scholar Google Scholar
https://scholar.google.com/scholar?q=how+to+trim+industrial+concrete+floors+cutting+grinding+finishing - Google Scholar Google Scholar
https://scholar.google.com/scholar?q=concrete+floor+edge+finishing+saw+cutting+and+grinding+procedure - Google Scholar Google Scholar
https://scholar.google.com/scholar?q=industrial+concrete+floor+grinding+safety+silica+dust+controls - Silica, Crystalline – Overview | Occupational Safety and Health Administration
https://www.osha.gov/silica - 1926.1153 – Respirable crystalline silica. | Occupational Safety and Health Administration
https://www.osha.gov/laws-regs/regulations/standardnumber/1926/1926.1153 - Silica and Worker Health | Silica | CDC
https://www.cdc.gov/niosh/topics/silica/ - https://pubmed.ncbi.nlm.nih.gov/?term=concrete+cutting+silica+dust+controls
- https://en.wikipedia.org/wiki/Concrete_cutting
- https://www.cdc.gov/niosh/topics/silica/default.html
- https://www.osha.gov/construction/silica-dust


